


TD-31040 Gas Spring Cylinder End Closing Machine | Tailgate Strut, Gas Lift, Shock Absorber

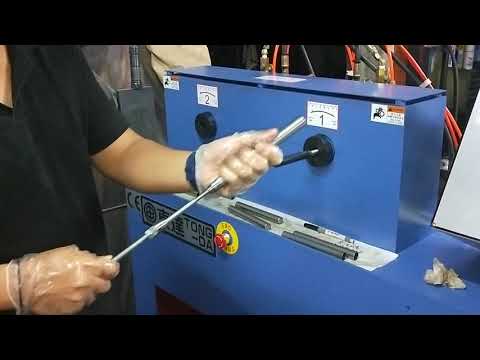


What a gas spring cylinder needs
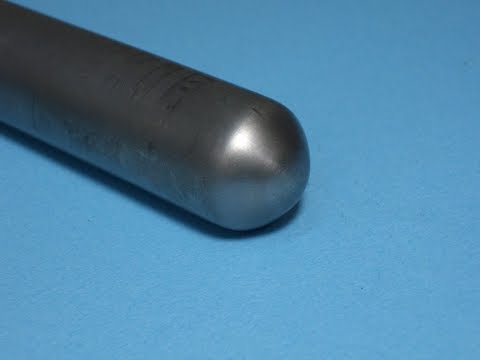
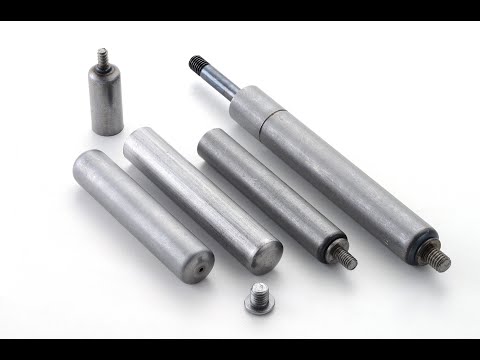
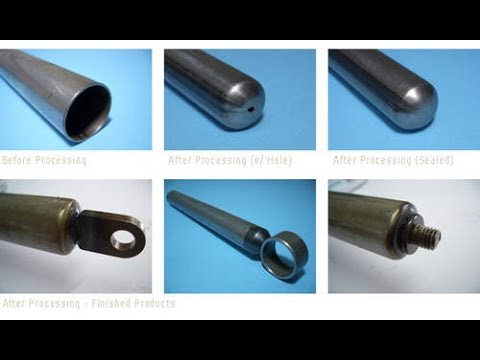
A gas spring cylinder is a precision steel tube worked at both ends: one end is closed (fully, or with a hole for an end fitting), the other is rolled over to retain the seal package and rod guide. The closed end must hold the charge pressure without leaking and ship with no further finishing. TD-31040 closes it in one cold roll-spinning operation; the wall thickens at the closure, so the end is stronger than the parent tube, with no weld and no plug.
Cylinder range
| Item | Spec |
|---|---|
| Cylinder OD | Machine range Ø10–40 mm; gas springs and shock absorbers typically Ø12–28 mm |
| Wall thickness | 0.8–2.0 mm |
| Materials | Cold-drawn precision steel tube, stainless steel, aluminum |
| Closed-end type | Fully closed dome; or dome with center hole set by tooling; adjustable dome radius |
| Standard jaw sizes | Ø12, 15, 18, 21, 22, 24, 28 mm and others on request |
Complete gas spring cylinder line from TONG DA
| Operation | Machine | Function |
|---|---|---|
| Cylinder end closing | TD-31040 | One-piece closed end or end with center hole |
| Inner grooving | TD-627 servo / TD-61530 | Oil grooves on the cylinder bore for damping and speed control |
| Component pressing and edge folding | TD-AT155 | Press in guide and seals, then roll the tube mouth over |
| Lock nut | TD-91528 | Tighten end screw or fitting |
| Edge folding and punching | TD-738 | Tube end folding and punching |
Machine features
- Three stations cycling in turn; one operator, short cycle time.
- Quick changeover: swap jaw and collet set and reset the stop for a new cylinder OD.
- PLC + touch screen, proximity-switch positioning for consistent hole size, batch counter with auto stop.
- Forced air cooling, no water circuit.
- 220–415 V, 3 phase.
Track record
Since 1989 TONG DA closing machines have shipped to gas spring and shock absorber makers in Germany, the USA, Japan, Turkey, India, Brazil and Thailand, with ongoing supply of jaws, collets and hydraulic chucks.
FAQ
Can both cylinder ends be done on this machine?
The closed end is done on TD-31040; the rod end pressing and roll-over is done on TD-AT155 or TD-738.
Can the closed end have a hole for a fitting?
Yes. The center hole diameter is set by tooling and kept consistent by proximity-switch positioning.
How many cylinder sizes on one machine?
Any OD from 10 to 40 mm by changing the jaw and collet set.
Trial closing?
Send tube OD × wall × material × length and the closed-end drawing; we trial-close and return samples.
*Sealing machine to process tube hardness have to less HRB55 and need enough ductility.
*Because it is a cold forming process, the tolerance will be unstable due to the factors of the pipe, and the tolerance of the incoming material will affect the overall tolerance. The tolerance of the incoming material must be as small as possible.
*Sealing machine to process tube weld bead have to firm, when sealed weld bead will not dehiscence.
*Outside dia less than 20mm, within length 1000mm can to install tube holder keep tube don't shake (need extra purchase).
*Stainless steel tube hardness is softer the better and good ductility, tube material weld bead have to firm.
*Tube outside dia and thickness have to collocation each other. Especially outside dia more than 25mm tube.
| 管徑大小 OD sizeψ(mm) | 3041B.3043B | |
| 最小管厚(mm) Min OD | 最大管厚(mm) Max OD | |
10~15 | 0.8 | 2.0 |
15~20 | 0.9 | 2.0 |
20~25 | 1.0 | 2.0 |
25~32 | 1.2 | 2.0 |
32~38 | 1.5 | 2.0 |
38~40 | 1.7 | 2.0 |
| Three Station-Tube Sealing Machine | Specification |
|---|
Patent Information:


Safety certification:
CE MARK


Partner company:
Sold to Germany gas spring factory , European, USA company, China, Thailand, Japanese car companies


