





Stabilizer Bar & Torsion Beam Production Line | Hollow Stabilizer Bar Tube Equipment


Hollow stabilizer bar end forming steps
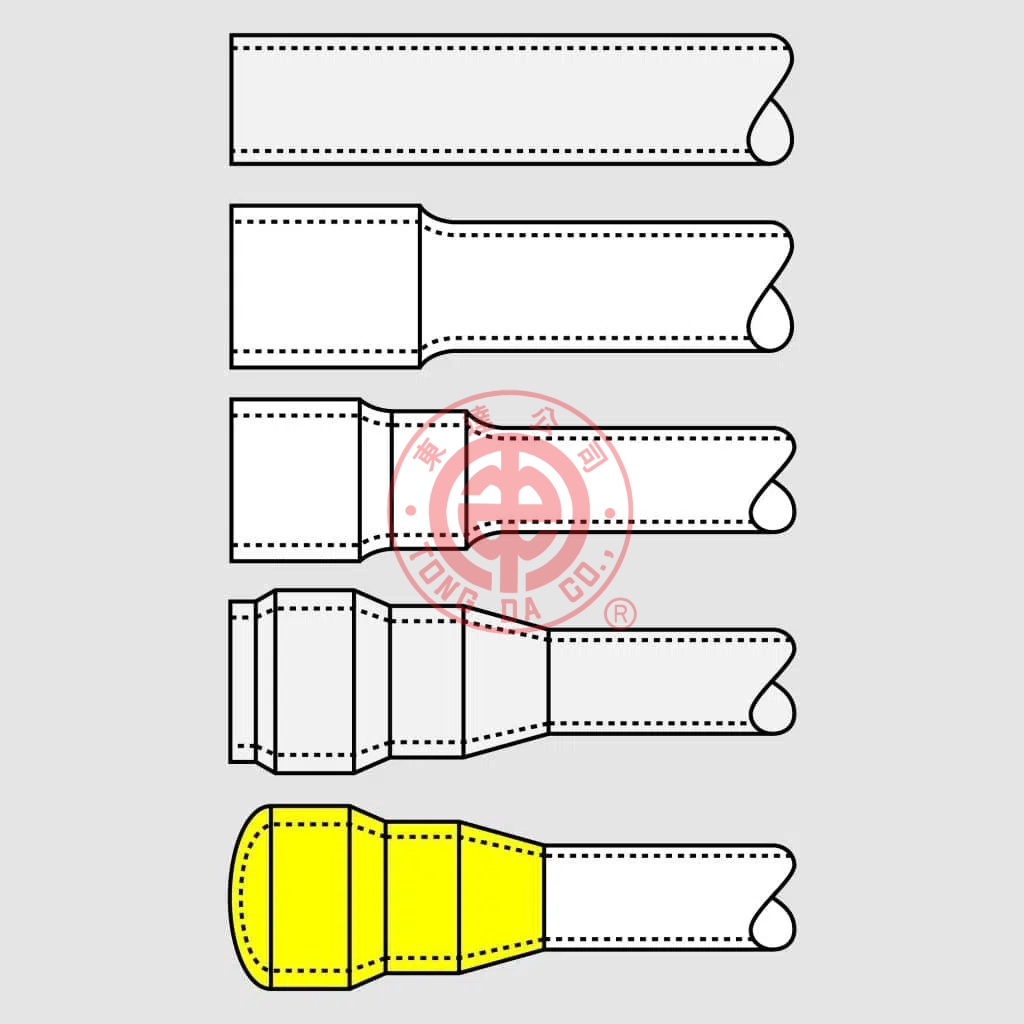
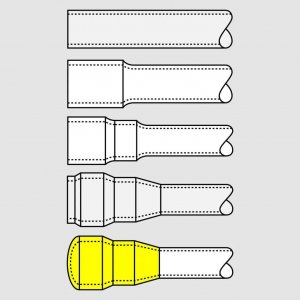
Both ends of a hollow stabilizer bar connect to links and bushings, so the tube end usually goes through several forming steps:
- Raw tube: welded or seamless tube, inner-drilled to remove the weld bead.
- Expanding: the tube end OD is expanded.
- Second expansion: a step is formed as a locating face.
- Multi-stage forming: upsetting, tapering and turning to the required shape and wall.
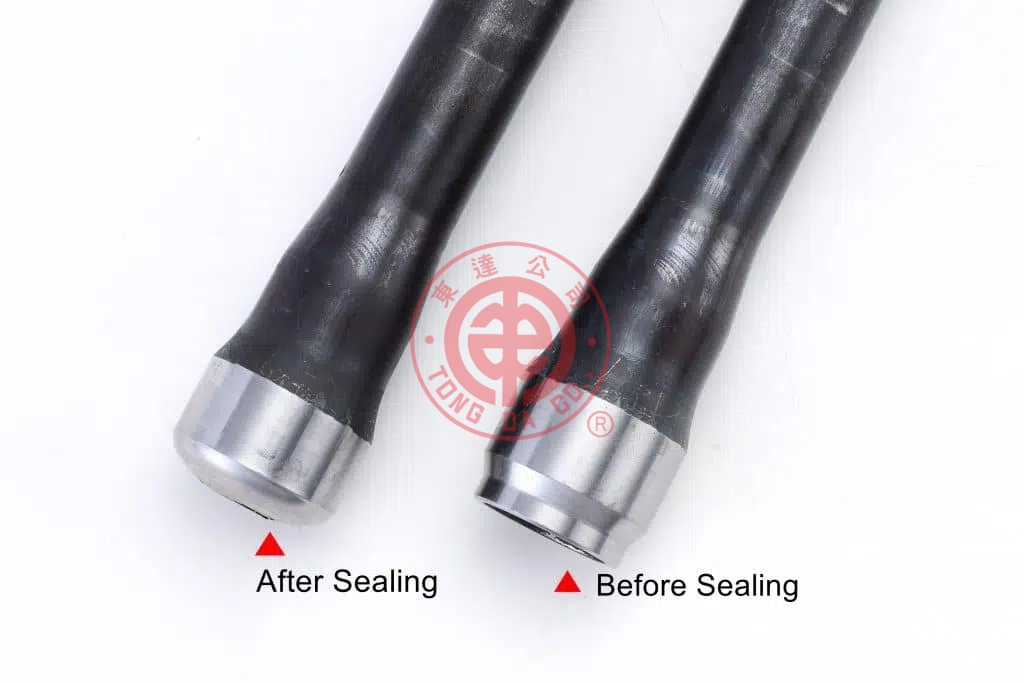
- End closing: finally the TD-382 NC closing machine spins the end closed, with dome and flat set to the drawing – no welded cap.
We can supply a single machine for one step or plan the complete line from drilling to closing around your drawing.
How to ask?
Email your stabilizer bar or torsion beam tube drawing to sales@tdco.com.tw.
Automobile Stabilizer Bar Related Equipment
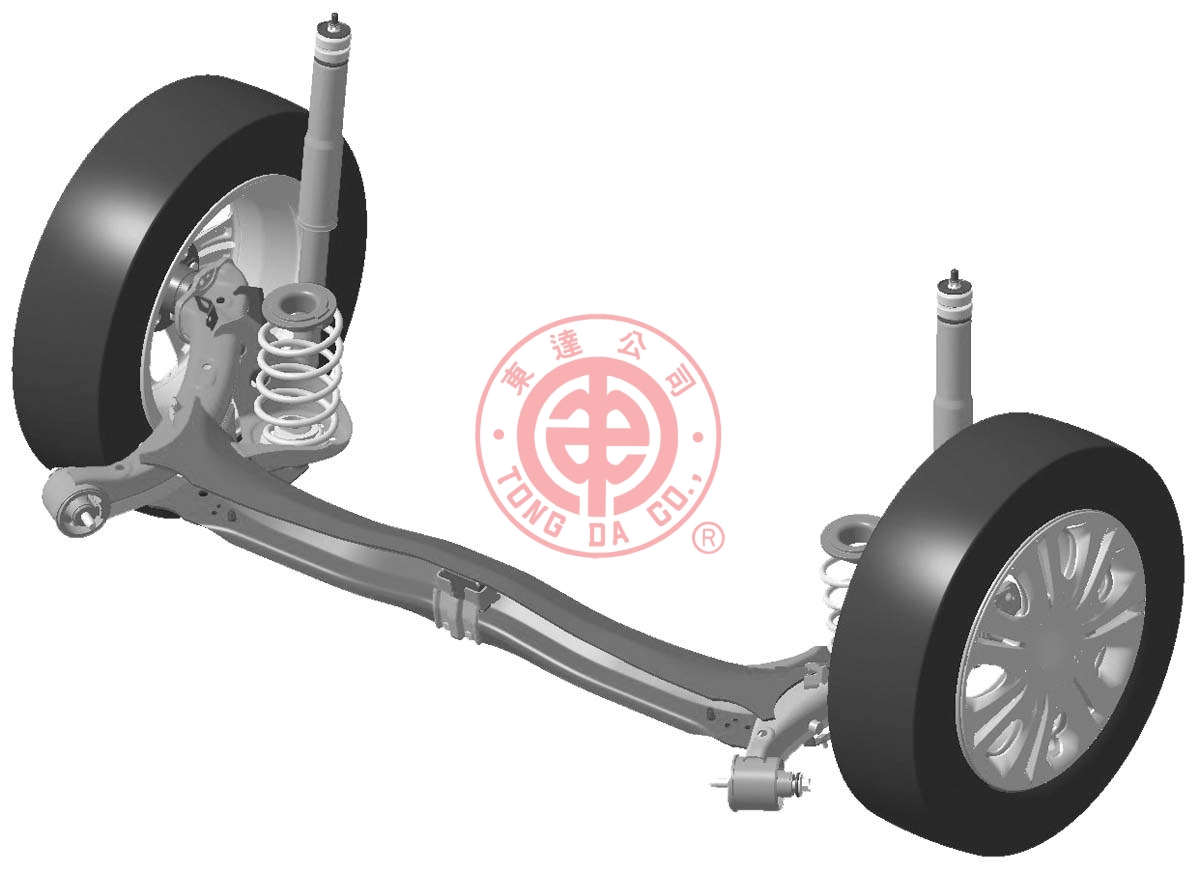
Design the whole plant equipment for automobile suspension buttons, torsion beams, torsion rod suspension rods, automobile balance shafts, stabilizers, and automobile balance rods, and have been exported to major international factories in Japan for mass production products.

1. Inner drill and engraving
(1) Sliding spindle head
(2) Manual feeding and automatic discharging
(3) Engraving bar codes for pipe fittings, drilling inner holes and engraving at the same time
(4) Utilization rate management software
(5) Numerical control and management of mechanical parameters (pressure/flow)


2. Pipe end expanding
(1) Standing clamp, lying punch
(2) Manual feeding and automatic discharging
(3) Two-stage punch
(4) Utilization rate management software
(5) Numerical control and management of mechanical parameters


3. Upset Forging
After high frequency, start to upset forging.
(1) Standing clamp, lying punch
(2) Manual feeding and automatic discharging
(3) Two-stage punch
(4) Utilization rate management software
(5) Numerical control and management of mechanical parameters


4. Lathe
(1)Follow your sample and drawing to design machine
(2) Machining steps: Load pipe, clamp, machining, complete.
(3) Advantage: Reduce labour use, increase machining speed and improve the
efficiency when producing which help customer reduce cost when making the final product.


5. Sealing
(1)Automobile stabilizer bar sealing
(2)Follow your sample and drawing to design machine
(3)Advantage: Reduce labour use, increase machining speed and improve the
efficiency when producing which help customer reduce cost when making the final product.


